The transitioning into a hygienically optimized production is the process of converting an existing food line so that equipment is easy to clean, drains freely and offers no hiding places for residue and microorganisms. Hygienic design here means equipment that is easy to clean, maintain and sanitise, built from suitable materials, without contamination traps and with proper drainage. This guide is written for plants and machine builders who cannot start from a blank sheet: it explains what to change first, what to leave for a rebuild, and how to prove each step worked.
Why the transition matters
Poorly cleanable equipment creates harbourage points – crevices (narrow gaps), dead spaces (areas cleaning flow cannot reach), lap joints and exposed threads where soil and microorganisms survive cleaning. They raise contamination risk and make it harder to show compliance with the regulatory framework, such as EU food hygiene and food-contact rules and US FDA requirements. They also cost time: every hidden area needs extra manual cleaning or dismantling.
For new machines, the machine builder's programme for hygienic optimisation covers training, standards and prototyping. This page deals with the line you already run.
Phase 1: Establish a baseline
- Map the zones. Mark the product-contact zone (surfaces product touches or drains back from), the splash zone (wetted by product spray or cleaning) and the non-contact zone.
- Record the cleaning method per zone: dry cleaning, foam and rinse, high-pressure washdown, or CIP/COP (cleaning in place without dismantling, or out of place after dismantling).
- Inspect after a normal cleaning cycle. Look under feet, around bolt heads, at seal edges, inside bearing housings, on frame ledges and at weld seams. Use swabs or ATP tests where your verification plan includes them.
- List the chemicals – alkaline, acid, chlorinated – with concentrations and temperatures.
- Rank findings by zone and by how often residue reappears.
The five design levers
The five levers from the original article remain the right framework. What changes in a transition is when you can pull each one.
| Lever | What good looks like | Retrofit or rebuild? | Typical trade-off |
|---|---|---|---|
| Material selection | Non-toxic, non-reactive, corrosion-resistant, compatible with cleaning chemicals; AISI 304 or 316L in wet areas | Component level now; structure at rebuild | 316L costs more but resists chloride pitting better |
| Design for cleanability | No crevices, seams or dead spaces; smooth, rounded surfaces; continuous, ground welds | Swap open-thread parts now; welds and joints at rebuild | Ground welds add fabrication time |
| Ease of disassembly | Quick-release fixings, removable guards and parts, all areas reachable | Often retrofittable on guards and guides | Loose parts must be controlled to avoid foreign bodies |
| Proper drainage | Sloped surfaces, no pooling, adequate drainage points | Mostly rebuild; tilt or replace flat covers now | Slopes take space and may change heights |
| Maintenance and inspection | Scheduled checks of seals, feet, bearings and surfaces | Immediately | Needs time on the cleaning schedule |
Material selection
Stainless steel is common because it resists corrosion, is durable and is easy to clean. The grade matters: in contact with salt, brine or chlorinated cleaners, AISI 316L resists chloride pitting (local corrosion pits started by chlorides) better than 304. After welding or machining, passivation restores the protective oxide layer. Mixing stainless steel with carbon steel or aluminium in wet areas invites galvanic corrosion. For seals and gaskets, the elastomer – EPDM, FKM or VMQ (silicone) – must suit the product (fats, acids) and the cleaning chemicals, and each food-contact material should come with a declaration of compliance under EC 1935/2004. See how chlorides and cleaning chemicals affect stainless steel machinery parts.
Design for cleanability
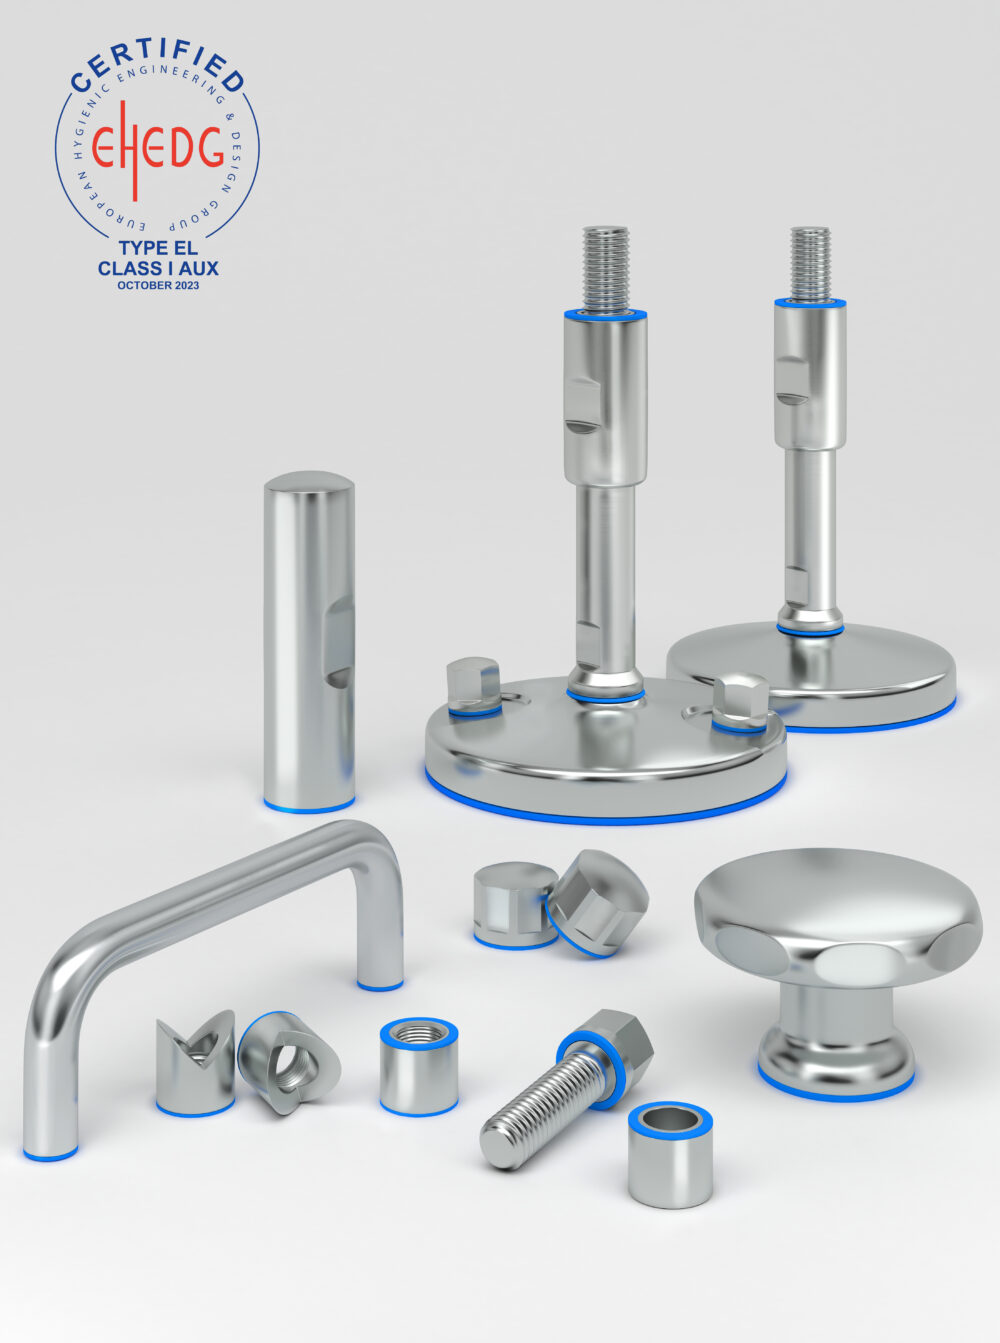
Minimise crevices, seams and dead spaces. Use smooth, rounded internal corners and proper welding: continuous welds, ground flush, instead of stitch welds or lap joints. EHEDG guidance refers to a surface roughness of Ra ≤ 0.8 µm (Ra = average roughness) for product-contact surfaces. In the splash zone, the quickest gains are usually components: sealed levelling feet without exposed threads, hygienic bolts with sealed heads, and sealed bearing units instead of housings with grease nipples and open gaps.
Ease of disassembly
Quick-release mechanisms and removable parts let cleaners reach every surface and allow inspection. The trade-off is control: removable parts must be designed so they cannot be lost into product or refitted wrongly.
Proper drainage
Water and cleaning solution that pool on flat surfaces harbour bacteria and accelerate corrosion. Sloped surfaces, self-draining profiles (that shed liquid by gravity) and enough drainage points prevent this. Structural slopes usually wait for a rebuild, but flat covers and brackets can often be replaced sooner.
Maintenance and inspection
A routine schedule catches worn seals, loosened feet and damaged surfaces before they become harbourage points. Include equipment checks in the cleaning verification, not as a separate activity.
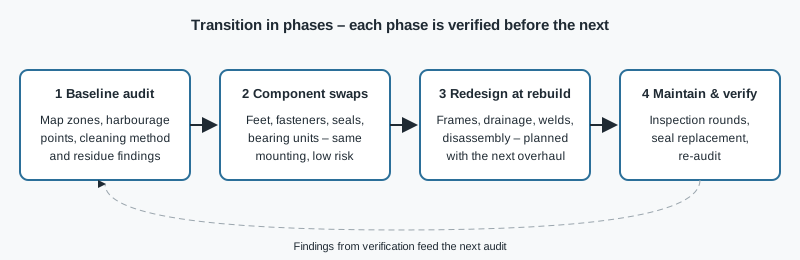
Phases 2–4: Swap, redesign, verify
- Phase 2 – component swaps: exchange parts that keep the same mounting during planned maintenance. Low risk, fast to verify.
- Phase 3 – redesign at rebuild: frames, drainage, welds and disassembly concepts, planned with the next overhaul or machine generation.
- Phase 4 – maintain and verify: repeat the post-cleaning inspection from Phase 1 and compare.
Example – assumptions stated, not a real plant. A dairy packing line shows recurring residue under the frame and around bolt heads in the splash zone; it is cleaned with foam and low-pressure rinse. Phase 2 replaces open-thread feet with sealed hygienic feet of the same thread size and load class, and hex bolts with hygienic bolts. Re-inspection after cleaning shows the foot and bolt findings gone, but water still stands on two flat cross-members. These go on the Phase 3 list for the next overhaul, with sloped profiles. The plant records cleaning time before and after each phase to judge the effect with its own numbers.
What to write in the specification
- Zone and cleaning method for each component (foam, washdown pressure and temperature, CIP/COP).
- Chemicals, concentrations and temperatures.
- Material grade (e.g. AISI 316L) and declarations of compliance for food-contact parts.
- Crevice-free, self-draining design; certified design only where a certificate for that design exists.
- Load, thread size and mounting must match the existing interface for Phase 2 swaps.
Failure modes to avoid
- Swapping parts on a frame that still pools water – fix drainage, or the gain is small.
- Choosing seals without the chemical list – they swell or crack at the plant.
- No baseline – without before-and-after data, nobody can show the transition worked.
- Quoting other plants' savings – measure your own.
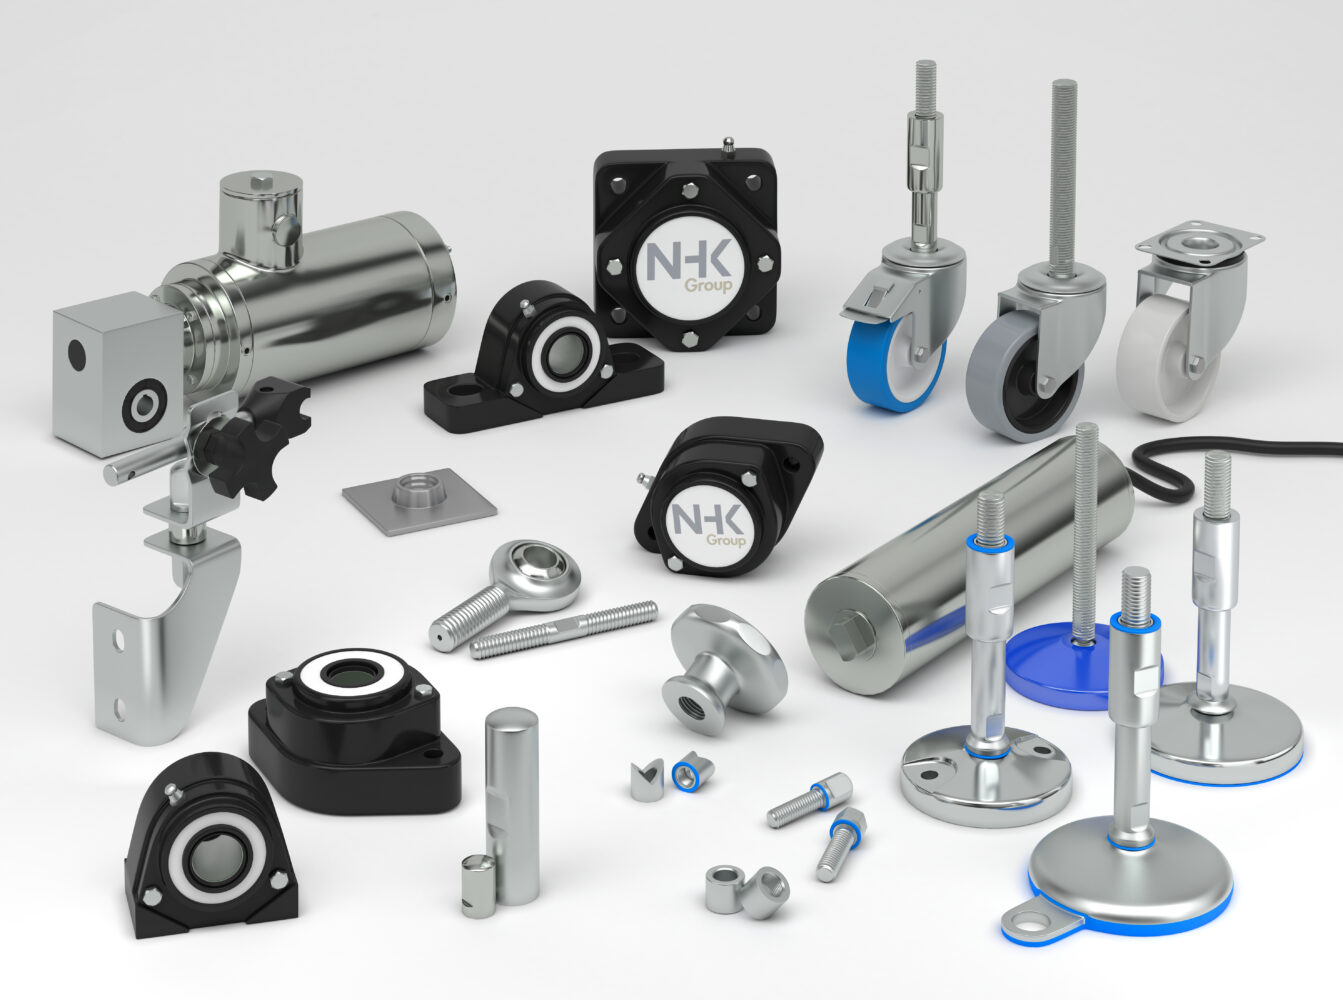
Product lines for stainless equipment, levelling castors and load feet and other components are listed at NHK Machinery Parts.
Conclusion
Move to hygienically optimized production in verified phases: audit, swap what fits, redesign what must, and keep inspecting. That turns hygienic design from a project into a property of the line.