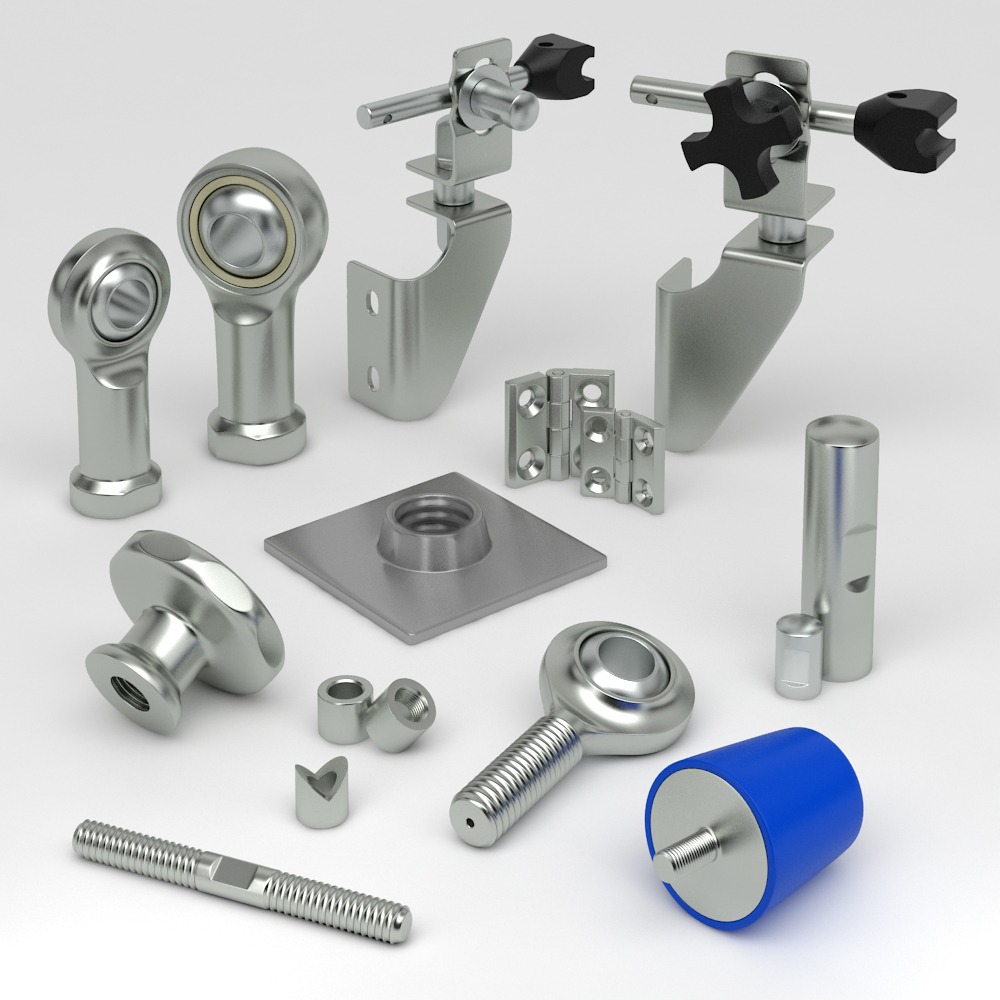
Hygienically optimized machine parts are components designed so that product residues cannot collect on them and cleaning reaches every surface. The idea applies to food processing, dairy, pharmaceutical and biotechnology machinery. This guide explains what optimisation means in practice for food processing parts, how requirements change by zone, and what to check before you buy.
What makes a food processing part hygienically optimized?
Four things decide whether a part is hygienic: design, material, surface and how it is installed and maintained.
- Design: no harbourage points – places where microbes can survive cleaning, such as crevices (narrow gaps), dead spaces (areas cleaning flow does not reach) and exposed threads. Surfaces are self-draining: water and detergent run off instead of pooling.
- Material: corrosion-resistant metals and food-contact-compliant plastics and elastomers.
- Surface: smooth enough to clean. EHEDG guidance refers to Ra ≤ 0.8 µm for product-contact surfaces; Ra (surface roughness) is the average height of the surface profile.
- Installation and maintenance: sealed mounting faces, correct torque, seals replaced before they crack.
The source article described food, pharma, dairy and biotech plants that reduced contamination with smooth surfaces, minimal crevices, self-draining designs, corrosion-resistant materials and better sealing. Those are exactly the four levers above.
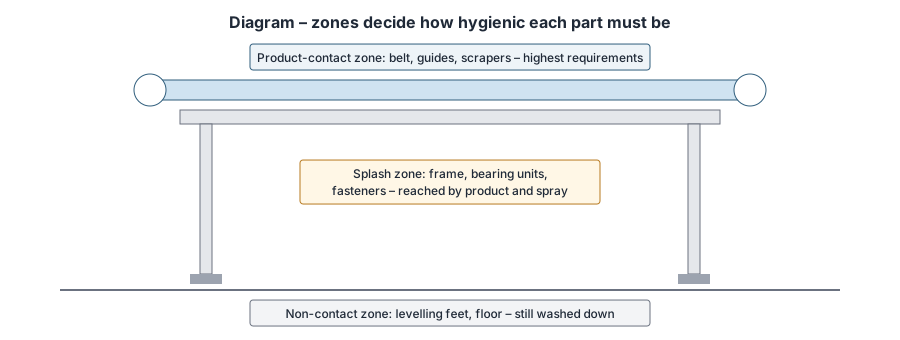
How hygienic does each part need to be? Set requirements by zone
How far to optimize depends on where the part sits:
- Product-contact zone: surfaces that touch food or from which liquid drains back onto it.
- Splash zone: surfaces reached by product splashes or cleaning spray that do not normally touch product.
- Non-contact zone: everything else, such as the floor area – still cleaned, often by high-pressure washdown.
Food machine parts: selection by part family
| Part family | Typical zone | Hygienic features to look for | Main trade-off |
|---|---|---|---|
| Guides, scrapers, belt supports | Product contact | Ra-controlled surfaces, rounded corners, food-contact plastics with declaration | Wear vs cleanability |
| Bearing units | Splash | Closed or sealed housing, no grease traps, stainless or plastic housing | Seal friction vs ingress protection |
| Fasteners | Splash/contact | Hygienic bolts with sealed head, no exposed thread | Higher part cost |
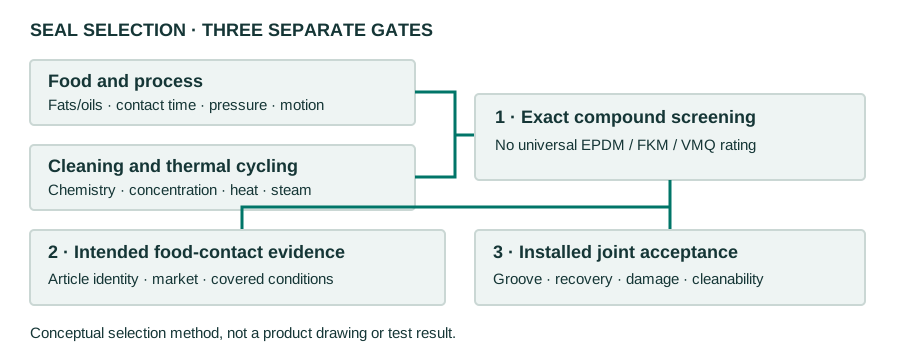
| Seals and gaskets | All | Elastomer compatible with fats and detergents (EPDM, FKM, VMQ) | Chemical vs temperature resistance |
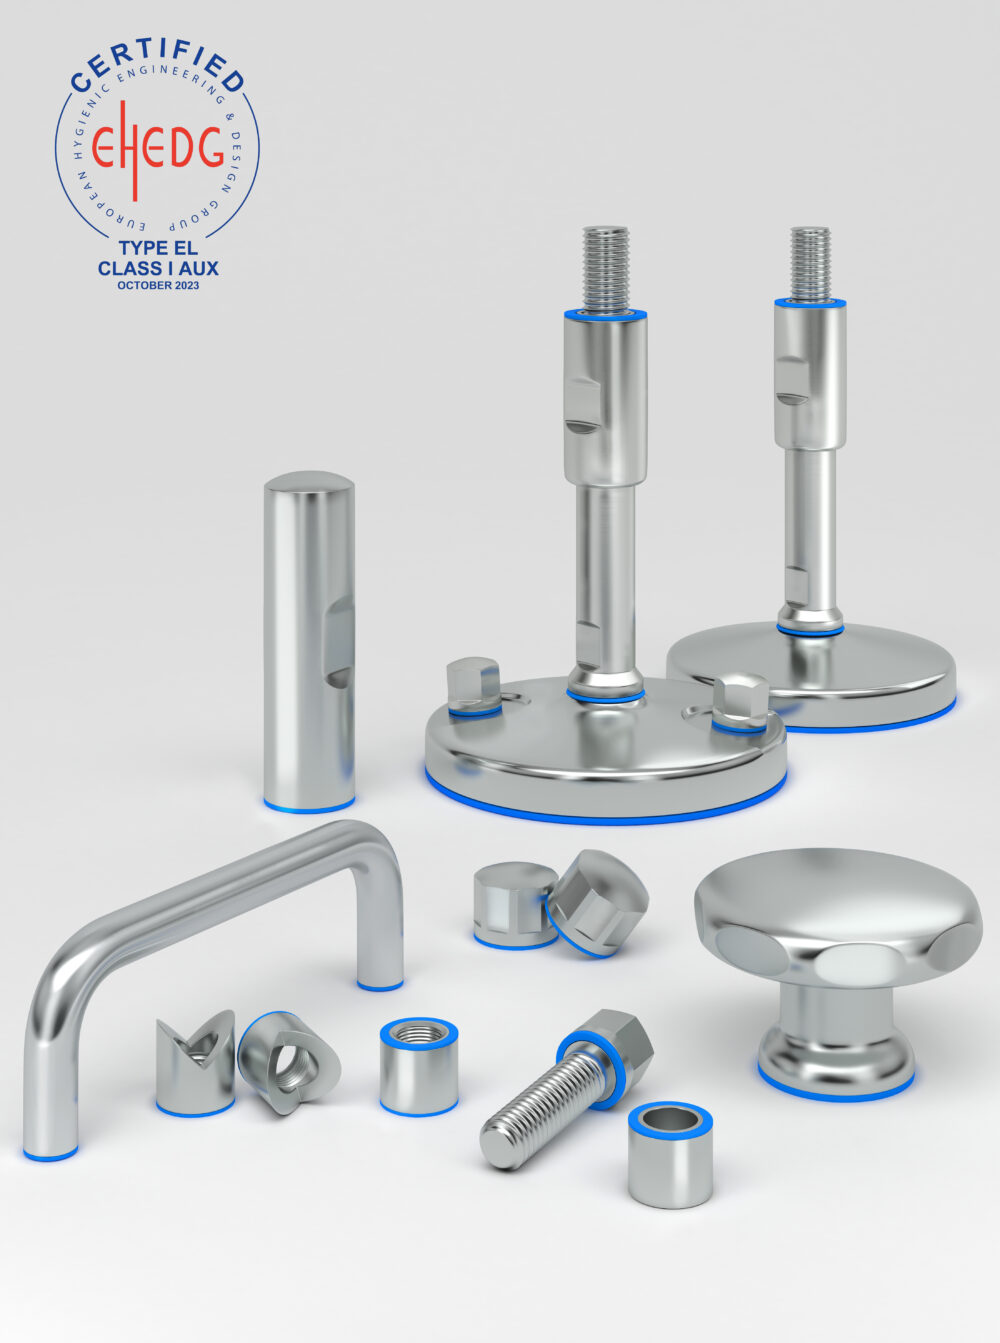
| Levelling feet (leveling feet) | Non-contact, washed | Sealed thread, no open gap at base, solid or sealed base | Adjustment range vs closed design |
| Castors | Non-contact, washed | Stainless frame, sealed bearings, cleanable wheel housing | Mobility vs cleanability |
Material choices for food processing machinery parts
For compliant stops and attachments, check rubber-to-metal interfaces and mounting duty separately from seals and rigid fasteners.
- AISI 304: standard stainless for dry and mildly wet areas.
- AISI 316L: molybdenum improves resistance to chloride pitting – local corrosion caused by salt, brine or chlorinated detergents.
- Plastics and elastomers: must comply with EC 1935/2004; plastics also with EU 10/2011; rubber for US markets with FDA 21 CFR 177.2600.
- Avoid mixed metals in wet areas – galvanic corrosion occurs where dissimilar metals touch in an electrolyte.
- Passivation: a treatment that restores the chromium oxide layer after machining or welding.
How to choose food processing parts: a method
- Map each part to its zone.
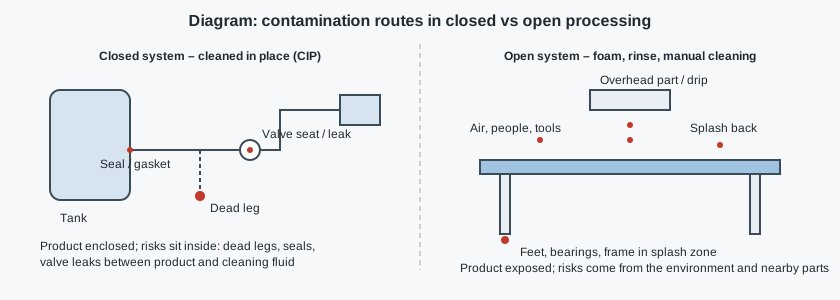
- Record the cleaning method: dry, foam, CIP (cleaning in place without dismantling), COP (cleaning out of place) or high-pressure washdown.
- List chemicals and temperatures used for cleaning and production.
- Choose the material grade and elastomer to match.
- Check design features: no exposed threads, no crevices, self-draining shapes.
- Decide whether a certified design (EHEDG or 3-A) is needed – usually for contact and splash zones with wet cleaning.
- Request documents and plan inspection intervals.
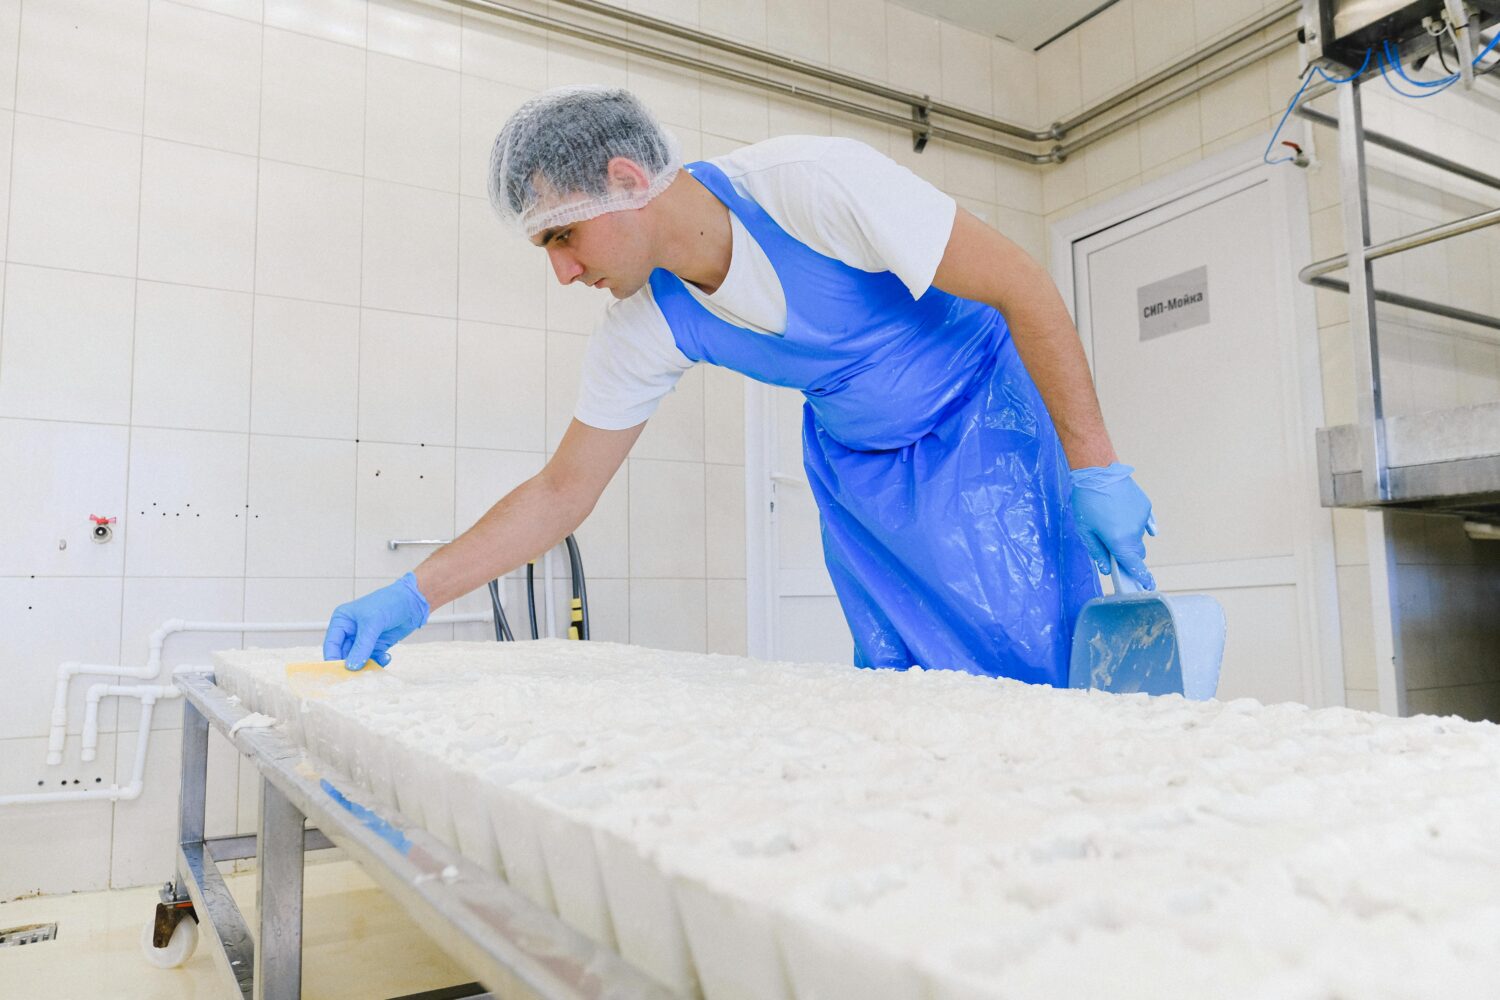
Example – assumptions stated, not data from a real plant. A cheese-portioning conveyor cleaned daily with alkaline foam and a chlorinated sanitiser. Guides are in contact with product, so they need food-contact plastic with a declaration. Bearing units and fasteners are in the splash zone, so sealed stainless designs in 316L because of the chlorine. Feet are washed by high-pressure hose, so sealed levelling feet without exposed threads. The motor cover outside the spray area can be a standard part.
What to write in an RFQ
For an unresolved interface, prepare a component question with drawings and cleaning data before choosing a part number.
- Zone and cleaning method for each part.
- Material grade (304 or 316L) and elastomer compound.
- Declaration of compliance under EC 1935/2004 (and EU 10/2011 for plastics).
- EHEDG certificate or 3-A authorisation for the exact model, if required.
- IP rating where relevant – IP67 is an immersion test and IP69K a high-pressure jet test; neither is a hygiene rating.
- Installation and cleaning instructions.
Failure modes and how to prevent them
- Exposed thread on feet or bolts collects soil: use sealed designs.
- Seal swelling or cracking: check elastomer compatibility with fats and detergents.
- Rust spots on 304 near brine: use 316L and avoid chloride residues.
- Water pooling on flat housings: choose sloped, self-draining shapes.
- Gaps at mounting faces: use hygienic gaskets and correct torque.
Inspection checklist after cleaning
- Look for residue at joints, thread runs and under feet and bearing housings.
- Check seals and gaskets for swelling, cracks or gaps at the edges.
- Check stainless surfaces for rust spots, pitting or discolouration near welds.
- Confirm water drains off horizontal surfaces and does not pool on housings.
- Check that fasteners and feet are still tight; loosened parts open new gaps.
- Record findings so repeat problems point to a part that needs a redesign, not more cleaning effort.
After an allergen changeover – switching production between products with different allergens – this check matters most, because residue on a single part can carry allergen into the next batch.
For general cleanability features, see easy-to-clean components and parts; for cleaning cost in total cost of ownership, see the importance of hygienic optimization. For how requirements differ by industry, see sanitary optimized parts and components.
Where to find hygienically optimized machine parts
NHK's range is listed under all product lines, including EHEDG certified and 3-A SSI standard components and stainless steel solid base feet. The relevant line for conveyor parts is conveyor components and machinery parts; contact NHK with your zone and cleaning data.