Automated hygienic components are sensors, actuators and machine parts that monitor or control processing and cleaning with less manual intervention, while following hygienic design principles. Demand for them is growing in food and pharmaceutical production as lines become more complex and hygiene requirements tighter. The benefits are real – repeatable cleaning, less human error, records for verification – but each added device is also a surface, a seal and a cable that must be cleaned.
This page covers where automation helps hygiene, how to integrate it without creating new harbourage points, and what to specify. For the broader picture of new component technologies, see innovations in hygienic design.
What counts as an automated or smart hygienic component?
| Type | Examples | Hygienic benefit | Hygienic risk if poorly designed |
|---|---|---|---|
| Process sensors | Temperature, pressure, flow, level, conductivity | Verifies CIP parameters and process conditions | Crevices at process connection, dead legs |
| Condition sensors | Bearing temperature, vibration | Maintenance planned before failure; fewer emergency openings | Sensors and brackets on non-contact surfaces collect soil |
| Automated valves and dosing | CIP valves, chemical dosing pumps | Repeatable cleaning, less manual chemical handling | Valve seats and actuators that are hard to clean |
| Automated cleaning systems | CIP skids, spray devices, automated washdown | Same cleaning every cycle, logged | Spray shadows, unverified coverage |
| Smart passive parts | Components with traceable IDs, wear indicators | Easier inspection and documentation | Labels and tags that peel or trap moisture |
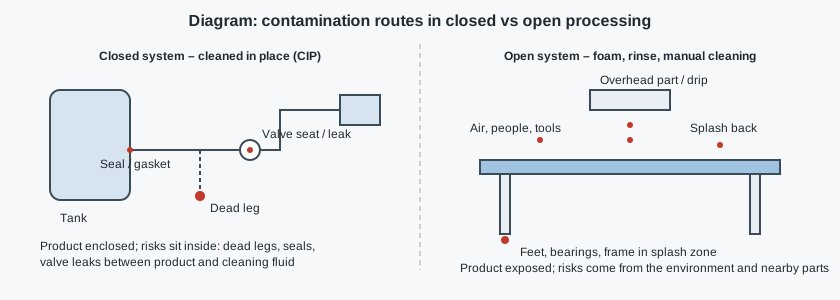
Harbourage points are places where residue and microorganisms survive cleaning. Dead spaces (dead legs) are areas outside the main flow where product or cleaning fluid stagnates.
Where automation actually helps hygiene
Fewer manual interventions
Every time an operator opens a guard, adjusts a part or dismantles a component, soil, allergens or microorganisms can be transferred. Automated adjustment, closed systems and sealed-for-life components reduce these contacts. The link between manual handling and errors is covered in 3-A sanitary design and human error.
Repeatable and verifiable cleaning
CIP (cleaning in place) circulates detergent and rinse water through closed equipment without dismantling it; COP (cleaning out of place) cleans dismantled parts in a washer. Automated CIP controls the four factors of cleaning – time, temperature, chemical concentration and mechanical action (flow) – and records them. Conductivity sensors confirm detergent concentration and rinse completion; temperature and flow sensors confirm each step ran as validated.
This gives a cleaning record that supports allergen changeover (cleaning between products with different allergens) and audit requirements. It does not prove the surface is clean: swabs, ATP tests or visual inspection still verify the result.
Condition-based maintenance
Bearing temperature and vibration monitoring can show deterioration before failure. That matters for hygiene because emergency repairs are a common moment for contamination: guards opened during production, tools and spare parts brought into the zone, cleaning skipped to restart. Planned replacement keeps work within the normal cleaning routine.
How to integrate sensors without creating harbourage points
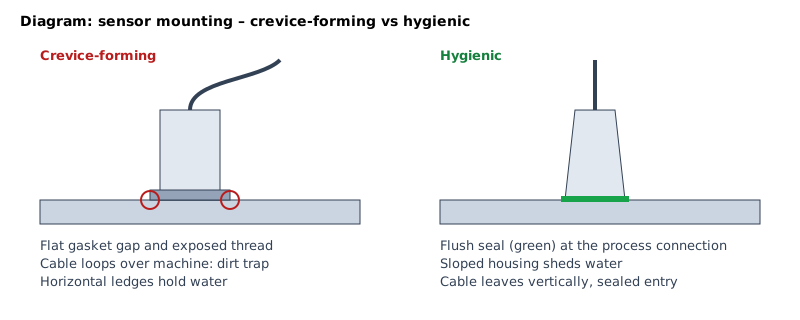
- Process connection: use hygienic connections with defined, flush seals – not threaded fittings with exposed thread or flat gaskets that leave a gap.
- Mounting position: avoid dead legs; mount sensors flush or with minimal insertion length, positioned so they drain.
- Housing shape: smooth, sloped or rounded housings that shed water; no horizontal ledges, recessed screws or labels that can peel.
- Cables: route vertically or on sloped trays, with sealed cable glands; avoid loops and bundles over product zones.
- Brackets: stand-offs from surfaces so the gap can be cleaned, or seal continuously – no tight metal-to-metal contact.
- Ingress rating: select for the cleaning method. IP69K (ISO 20653, high-pressure water jet) is a useful indicator for washdown zones; IP67 is an immersion test (IEC 60529) and not a washdown rating. Neither is a hygiene certification – see IP68 or IP69K in hygienic zones.
Materials for automated hygienic components
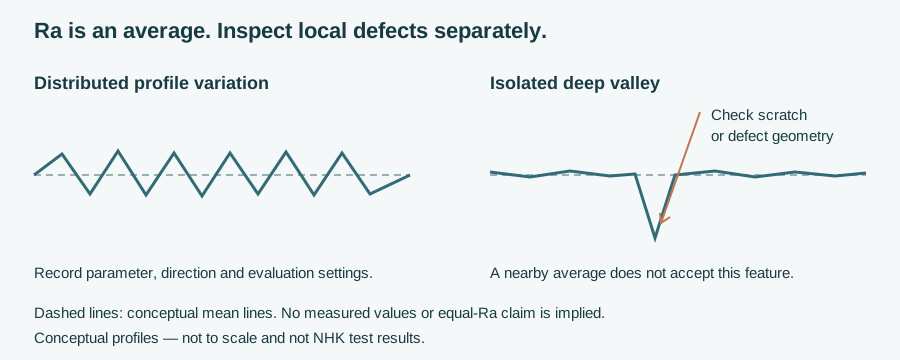
- Stainless steel (AISI 304, or 316L where chlorides are higher) for housings and process-wetted parts: corrosion resistant and cleanable. Surface finish matters – EHEDG guidance gives Ra ≤ 0.8 µm for product-contact surfaces. Surface roughness Ra is the average deviation of the surface profile from its mean line.
- Food-grade plastics for housings, covers and some valve parts where stainless is not needed or not suitable. Check temperature limits and resistance to cleaning chemicals; in the EU, plastics in food contact fall under EU 10/2011 as well as EC 1935/2004.
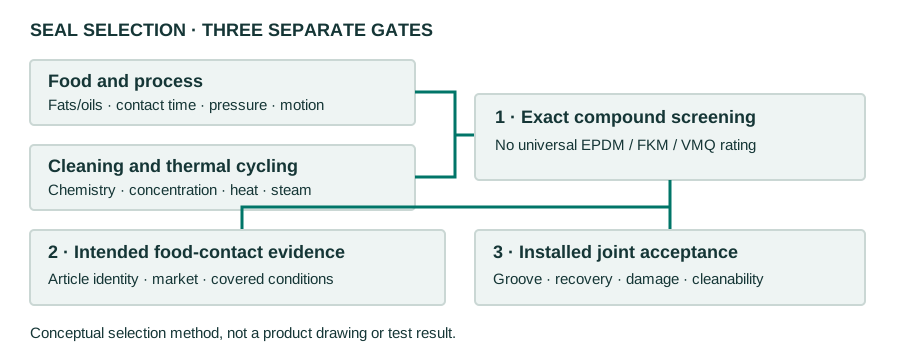
- Elastomers for seals and gaskets: flexible and able to seal tightly, but each has limits. Check elastomer compatibility – EPDM suits hot water and steam but not oils and fats, FKM suits oils and many chemicals, VMQ (silicone) suits wide temperature ranges but has lower mechanical strength. In the US, rubber in food contact is covered by FDA 21 CFR 177.2600.
Ask for a declaration of compliance – the supplier's written statement that a food-contact material meets the applicable regulations – for every food-contact material.
EHEDG and 3-A for automated components
EHEDG and 3-A apply to automated components the same way as to any other part:
- EHEDG certifies specific equipment designs after review against its guidelines and, for many closed components, a cleanability test. Certificates are listed in the EHEDG database.
- 3-A Symbol authorisation confirms a specific design meets the applicable 3-A Sanitary Standard, following a Third Party Verification.
- Both are voluntary, and neither covers a whole company or range. A sensor brand with one certified design does not make all its sensors certified.
Comparison of the two schemes: what is the difference between 3-A and EHEDG. Examples of certified designs: EHEDG and 3-A components.
Industry differences
- Dairy: extensive CIP of closed systems; 3-A is widely referenced; temperature and conductivity verification is central.
- Meat and poultry: open equipment with daily high-pressure and foam washdown; sensors, cables and enclosures need washdown-suited designs and sealed entries.
- Beverage: mostly closed systems with CIP; flow and concentration monitoring dominate.
- Pharmaceutical and nutraceuticals: documentation, traceability and validated cleaning; data integrity of cleaning records matters as much as the hardware.
What to write in a specification or RFQ
- Zone (product-contact, splash or non-contact) and cleaning method (CIP, COP, foam, high-pressure washdown).
- Cleaning chemicals, concentrations and temperatures.
- Hygienic process connection type and seal material.
- Material grade and surface finish (Ra) for wetted and splash surfaces.
- Ingress rating required for the cleaning method.
- EHEDG certificate or 3-A authorisation number, if required – for the exact model.
- Declarations of compliance for food-contact materials.
- Signals and data to be recorded, and how they feed the cleaning record.
Example: adding bearing monitoring to a washdown conveyor
Assumptions (illustrative): a poultry conveyor with stainless bearing units, daily foam cleaning, unplanned bearing failures several times per year.
- Choice: sealed stainless bearing units with temperature monitoring, sensor housing sloped and sealed, cable routed vertically to a sealed gland.
- Decision rule: a rising temperature trend triggers replacement at the next planned cleaning stop, not during production.
- Hygiene effect: repair work moves out of production; no extra horizontal surfaces or loose cables added.
- Check: confirm the sensor housing and cable materials resist the foam detergent before rollout.
The automation only works on mechanically hygienic base components. Sealed bearing units, hygienic feet and crevice-free fasteners remain the foundation – see the range of hygienic components.