Machinery components are the bearings, leveling feet, castors, conveyor parts, seals and fasteners from which production machines are built – and their contribution to manufacturing success is best measured as total cost of ownership rather than purchase price. Understanding how components affect a machine and why the right choice pays back helps engineers and buyers defend a decision that looks more expensive on the quote.
This page gives a practical total cost of ownership (TCO) method for component decisions. For the reliability and maintenance side, see optimizing industrial machinery performance; for the selection steps, see industrial machinery parts and components.
How machinery components affect efficiency and performance
Every component on a machine influences efficiency, safety and service life:
- Bearings, pulleys and sprockets give smooth, low-friction motion. A worn or misaligned bearing raises friction, temperature and energy use before it fails.
- Machine leveling feet carry and stabilise the machine. A rocking frame transmits vibration that wears bearings and drives and affects weighing, cutting and filling accuracy.
- Seals and housings keep water, dust and product out. In washdown zones they decide whether a bearing lasts years or months.
- Precision-made parts with controlled tolerances fit correctly, which reduces installation errors and early wear.
How components cause downtime
Downtime means production delay, lost output and, in food plants, product at risk. The usual component causes are water and detergent ingress, corrosion, lubricant washout, overload and misalignment. Durable materials (stainless steel, engineering plastics), effective sealing and correct installation address most of them.
How hygienic design affects cost in food plants
In food, dairy and pharma production, cleaning time is lost production time. Components with exposed threads, crevices or flat surfaces take longer to clean and are more likely to harbour residue. Harbourage points – places where residue and microorganisms survive cleaning – also raise the risk of failed hygiene checks and product holds. Hygienic designs with sealed joints and self-draining surfaces reduce both.
Why the purchase price is the wrong measure
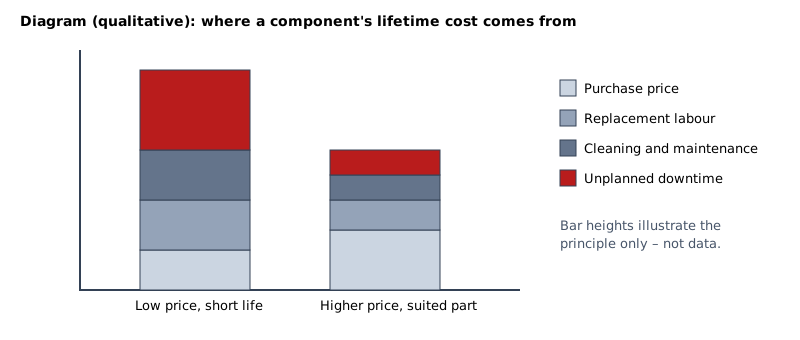
Low-cost components can lead to:
- Frequent replacements: each one costs a part, labour and often a production stop.
- Higher energy use: worn or poorly made bearings and belts create extra friction.
- Unexpected failures: sudden breakdowns that cannot be planned into a cleaning or maintenance window.
The purchase price is often the smallest part of a component's lifetime cost. The diagram shows the principle; the proportions depend entirely on the application.
What "high quality" means
"High quality" is not the same as "most expensive". It means suited to the application:
| Factor | Question to answer | Example of a mismatch |
|---|---|---|
| Load | Does the rating cover the real load with margin? | Feet sized on total weight ÷ number of feet, ignoring uneven floor |
| Environment | Wet, washdown, chemicals, temperature? | Painted cast iron bearing housing in daily washdown |
| Cleaning method | Dry, foam, high-pressure, CIP? | IP67 part where high-pressure spray is used |
| Material | Does it resist the chlorides and detergents? | AISI 304 where chlorinated disinfectant pools |
| Hygiene zone | Product-contact, splash or non-contact? | Exposed thread in the splash zone |
| Access | How hard is replacement? | Bearing behind a guard needing two hours to reach |
A splash zone is an area where liquid or product can splash and return to the product. Chloride pitting is local corrosion of stainless steel caused by chlorides – AISI 316L resists it better than AISI 304.
How to calculate total cost of ownership
- Define the period: usually the expected machine life or a planning horizon.
- Purchase cost: unit price × quantity.
- Number of replacements: period ÷ expected service life in this application (from experience, supplier data or a life calculation).
- Replacement cost: per replacement, parts + labour hours × labour rate.
- Downtime cost: for failures that stop the line, stop duration × cost per hour of lost production.
- Cleaning and maintenance cost: extra cleaning minutes per day caused by the part × days × labour rate; plus lubrication or inspection time.
- Add up and compare options. Note which inputs are estimates.
TCO = purchase + (replacements × replacement cost) + (unplanned stops × downtime cost) + cleaning and maintenance cost
Example: bearing units on a washdown conveyor
Assumptions (illustrative, not product data): 5-year horizon; 8 bearing units; daily foam cleaning; downtime cost and labour rate set by the plant.
- Option A – low-cost painted housing: fails from water ingress roughly once a year per position in this environment (plant experience). Over 5 years: about 40 replacements, many of them unplanned stops.
- Option B – sealed stainless or composite housing: expected to last the 5-year horizon in this environment; maybe a few replacements at planned stops.
- Comparison: even if Option B costs several times more per unit, the difference in replacement labour and unplanned stops will usually outweigh it. Enter the plant's own downtime cost and labour rate to get a number.
The value is less in the result than in the discipline: the assumptions become visible and can be checked against real failure records.
Why certifications and ratings matter – and what they prove
Use each for what it actually covers:
- EHEDG: certifies specific equipment designs against hygienic design guidelines. Voluntary.
- 3-A Symbol authorisation: confirms a specific design meets a 3-A Sanitary Standard after Third Party Verification. Voluntary.
- IP67 / IP69K: ingress tests. IP67 (IEC 60529) is immersion, not washdown; IP69K (ISO 20653) tests high-pressure, high-temperature water jets. Neither is a hygiene certification.
- ISO 9001: the supplier's quality management system, not the product.
- RoHS and REACH: restrictions on hazardous substances; RoHS covers electrical and electronic equipment.
- Food-contact compliance: EC 1935/2004 in the EU (plus EU 10/2011 for plastics); FDA rules in the US, such as 21 CFR 177.2600 for rubber. Ask for a declaration of compliance.
A certificate reduces risk only when it applies to the exact part in the exact application.
How to match components to the industry
- Food and beverage: hygienic, corrosion-resistant parts such as stainless steel leveling feet and sealed bearing units; cleaning method decides seals and ingress rating.
- Pharmaceutical and biotech: cleanable, documented components with food- or pharma-grade materials and traceability; validated cleaning.
- Heavy machinery and automotive: high-load bearings and vibration-resistant parts; hygiene less important, load and precision dominant.
Materials: stainless steel AISI 304 or 316(L) for hygienic and corrosive environments; engineering plastics such as POM and UHMW-PE for low-friction conveyor parts; aluminium for light automation frames, but avoid it where alkaline detergents are used.
Why supplier reliability matters
A component is only as reliable as its supply. Check:
- Consistent quality: material certificates, traceability, stable specifications between batches.
- Delivery: stock and lead-time information for spare parts.
- Technical support: answers to load, chemical and cleaning questions, not only catalogue references.
- Documentation: datasheets, certificates for specific designs, declarations of compliance.
For the publisher of this site and its verified product groups and certificates, see NHK Machinery Parts.
Innovations worth considering
Condition-monitoring sensors on bearings, modular conveyor systems and wear-resistant coatings can lower TCO further – if the sensor or coating suits the environment and the data changes a decision. See innovations in hygienic design for how to evaluate them.
For an overview of the component groups available from NHK Group, see industrial machinery.
For a component-level break-even method and RFQ checklist, see ensuring long-term cost savings and competitive edge.