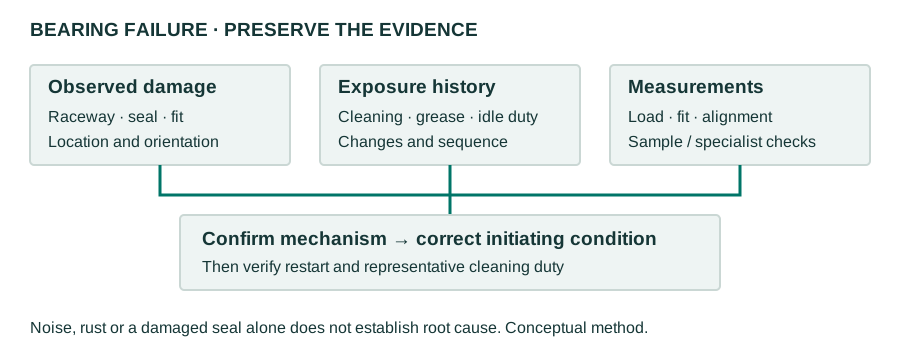
Preventive vs predictive maintenance is a choice between scheduled intervention and action based on evidence of developing failure. For food machinery, use both where justified: planned hygiene and safety checks remain mandatory even when vibration or temperature trends look normal. Start with the bearing damage and exposure investigation if a component is already deteriorating; monitoring is not a repair.
Preventive vs predictive maintenance: compare the triggers
Preventive maintenance uses planned time, operating hours or cycles to trigger defined work. Predictive maintenance uses condition data and analysis to anticipate deterioration and plan intervention. Condition-based maintenance responds to measured condition; it becomes predictive when the interpretation supports a forecast, rather than merely reporting an alarm.
| Decision | Preventive maintenance | Predictive maintenance | Washdown implication |
|---|---|---|---|
| Work trigger | Approved schedule or usage count | Trend, diagnostic evidence and forecast | Cleaning-event checks can complement either strategy |
| Best fit | Known wear pattern, required inspection, simple accessible items | Critical rotating assets with measurable deterioration | Match sensor method to speed, duty and installed access |
| Evidence needed | Unit instructions, exposure and maintenance history | Repeatable baseline, comparable measurements and diagnostic expertise | Compare equivalent load, speed and time since cleaning |
| Main limitation | Calendar replacement can be premature or miss rapid failure | Some failure modes are sudden or poorly observable | Neither method proves hygiene acceptance |
| Typical task | Check covers, support, wheel condition or approved grease service | Trend vibration and investigate a developing bearing defect | Retain exterior seal, drainage and contamination checks |
Send your application data and get a component recommendation
Choose scheduled inspection for castor brakes, loose covers, support movement and contamination paths that need a physical check. Consider predictive analysis for a production-critical conveyor bearing when a developing defect can be detected reliably and the plant can act before failure. A sensor is not useful simply because it generates data: decide which defect it detects, who interprets it and what action follows.
Preventive maintenance in food processing: set inspection intervals
There is no universal daily, weekly or monthly service interval for bearings, feet or castors. Establish the starting schedule from the exact manufacturer's instructions, machine risk assessment, cleaning exposure and plant records. Separate inspection frequency from replacement frequency and lubrication frequency; they answer different questions.
- Identify the asset and zone. Record unit designation, machine position and whether it is in a product-contact, splash or non-contact zone. A splash zone receives spray without intended direct food contact, but grease or fragments may still transfer toward food.
- Describe duty and exposure. Record speed, load, operating hours, starts, idle vibration, washdown method, chemical concentration, temperature, dwell and rinse. A changed cleaner or nozzle arrangement is a review trigger, not a reason to reduce sanitation without QA agreement.
- Define each task and checkpoint. State whether the check is visual, functional, dimensional or instrumented, its safe working state, and the acceptance criteria from the drawing, unit instructions or validated plant procedure. “Check bearing” is not a complete work order.
- Assign scheduled and event-driven checks. Plan inspections at suitable shutdown or hygiene-release opportunities. Add checks after impact, relocation, seal replacement, changed cleaning or an abnormal trend. Event checks do not silently replace required routine work.
- Review the evidence. Record defects and clean inspections, not only completed tickets. Shorten an interval when deterioration appears before the next check; extend it only through documented risk review, within supplier and regulatory constraints. Record who authorised the change.
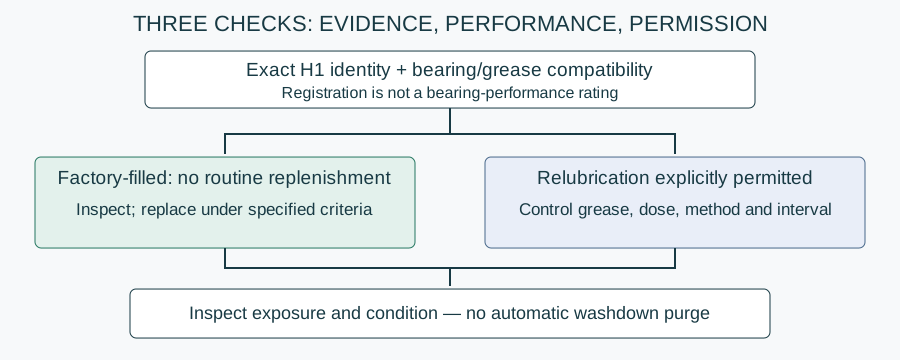
For lubrication tasks, use the grease identity and servicing-permission checks. Factory-filled units still need condition inspection, while relubricable units need the specified grease, dose, method and interval. More frequent greasing is not a universal response to washing and can introduce contamination or displace seals.
What to check on bearing units, levelling feet and castors
Levelling feet and castors deserve their own inspection points: a bearing vibration route will not reveal a loose floor anchor or an ineffective wheel brake. Make machinery safe, secure supported loads and follow isolation procedures before touching shafts, wheels or supports. Running measurements require an engineered safe-access arrangement, not improvised reach past guarding.
| Component | Inspection points | Evidence to record | Stop or escalate when |
|---|---|---|---|
| Bearing unit | Cover seating, shaft-side seals, leakage, housing joint, noise and measured trend | Position, operating state, photographs, comparable vibration/temperature readings | Seal displaced, cover loose, rapid condition change or contamination route identified |
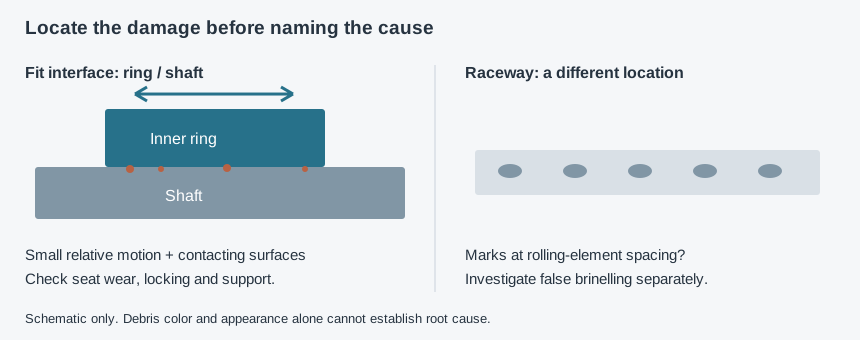
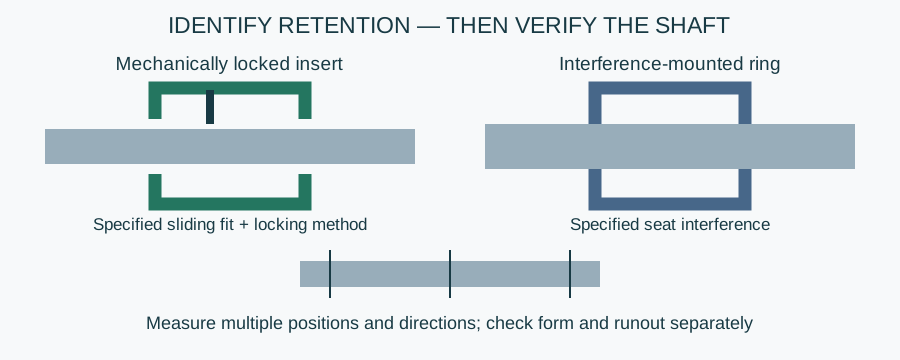
| Bearing mounting | Locking arrangement, support, fasteners and seat movement | Drawing limits, alignment, fit measurements and debris location | Movement, distortion or damaged seat exceeds approved acceptance |
| Levelling foot | Stem seal, base contact, anchor, load path and liquid retention | Position, stability, joint condition and installation record | Machine rocks, anchor loosens, seal cracks or support is damaged |
| Castor | Tread, wheel rotation, swivel, axle, brake and fixing | Unloaded/loaded test conditions where safe, debris, flat spots and brake function | Brake cannot restrain intended movement, wheel binds or tread separates |
| Hygiene interfaces | Residue beneath housings, covers, feet and wheel forks | Cleaning access, drainage and QA findings | Residue remains or escaped grease/fragments threaten product |
Do not retighten locking screws or anchors blindly when movement appears. Establish the cause and use the specified procedure; repeated tightening can conceal a worn seat or damage a support. The shaft-seat measurement and locking-system route separates fit acceptance from an assumption that more torque solves movement.
For brake function, consult the wheel, swivel and floor-lock comparison. A wheel brake and a swivel lock restrain different motion; verify the actual arrangement under its permitted duty. Remove wrapped film, string or product debris through the approved procedure rather than treating rising push force as proof of bearing wear.
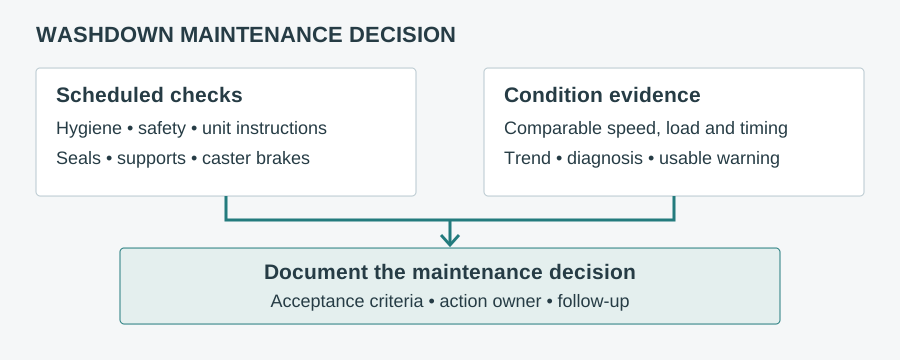 Scheduled hygiene and safety checks remain in place; condition evidence adds a separate decision route. Maintenance schematic, not an NHK product or performance result.
Condition monitoring: measure a repeatable signal
Condition monitoring tracks measurable indicators of machine health. ISO 17359, Condition monitoring and diagnostics of machines — General guidelines, provides the general programme framework; it does not prescribe a universal alarm or inspection interval for every food-plant bearing.
Vibration can reveal developing mechanical defects where speed, load, sensor location and signal processing suit the asset. Temperature supports trend assessment but also changes with ambient conditions, load, lubrication and recent hot cleaning. Ultrasound or lubricant analysis may add evidence where the unit and access allow a valid measurement. No single method identifies every failure cause.
Establish a baseline after accepted installation and representative operation. Record sensor mounting, direction, speed, load and measurement settings. Compare readings at equivalent operating conditions and a documented point relative to washdown. A hot housing immediately after sanitation should not be compared uncritically with a cool production baseline.
Install sensors, cables and brackets without creating harborage points—locations that retain residue through cleaning—or defeating seals and guards. Confirm cleanability, chemical compatibility and the applicable ingress evidence for the installed assembly. IP67 under IEC 60529 is a temporary-immersion test, not a pressure-wash rating or hygiene certificate.
When does predictive maintenance pay off?
Predictive maintenance suits critical assets with observable deterioration, repeatable measurements and response capacity. Retain physical checks for defects without reliable warning; for load changes, use the fatigue-versus-static capacity assessment.
Assess a detection-to-action window: the usable time between a reliably observable defect and unacceptable failure under actual duty. This is sometimes discussed as the potential-failure-to-functional-failure, or P–F, interval. It is not a fixed bearing-life value; use supported evidence and uncertainty rather than declaring a universal fraction as the inspection schedule.
Compare annual monitoring cost—hardware, hygienic installation, analysis, training and follow-up—with the expected avoidable failure cost based on plant records. Include false alarms, missed defects and planned interventions. Do not count all historical downtime as avoidable: sanitation and failures unrelated to the monitored signal do not become savings automatically.
Use the migrated downtime categories and cost-assessment method as a record structure, not a promised saving. No maintenance-strategy calculator is currently published on this site; use the buyer’s evidence and application guides to organise a documented proposal.
In the related corrosion cluster, use the cleaner exposure and corrosion-identification route to distinguish metal attack from mechanical wear.
How hygienic components change the maintenance plan
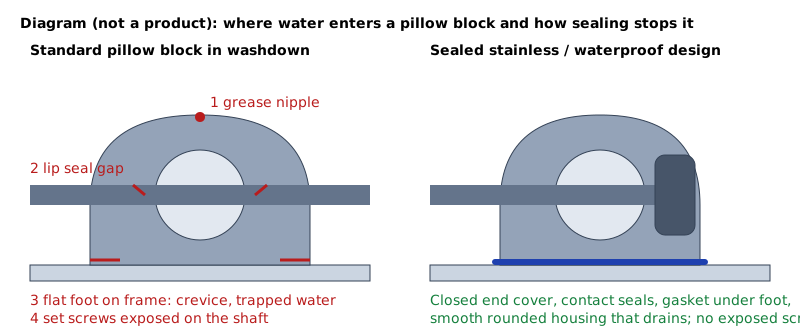
A cleanable exterior and protected interfaces can change access, inspection points and required interventions, but do not remove maintenance. When replacing an exposed arrangement with a sealed one, document which surfaces remain inspectable, how covers are verified and whether the lubrication strategy changes. Do not transfer the old grease routine to a different unit automatically.
For changed hygiene zones, follow the low-risk to high-risk machinery conversion guide.
The migrated bearing housing and cleaning-access guide provides design context; actual unit instructions govern servicing permission and cleaning limits. In the related cleaning cluster, use the installed residue-removal and access checks to assess hidden joints. CIP means cleaning in place; COP means cleaning removed parts. Neither label proves a covered bearing joint is clean.
NHK lists machine support options for an inspection-plan review and stainless castor arrangements for maintenance-access checks. Request exact-item installation and service instructions. This guide makes no category-wide claim about grease life, cleaning endurance, loads or a maintenance-free design.
Example: choose a mixed strategy for a washdown conveyor
Example — hypothetical assumptions, not NHK field data. A conveyor has production-critical bearing units, adjustable supports and a movable auxiliary frame. Cleaning occurs between batches, but no validated defect-to-failure interval is available. Bearing readings can be taken safely at repeatable production conditions; wheel and support defects are assessed physically.
Retain planned seal, drainage, support and brake checks at the approved inspection opportunities. Pilot bearing measurements with recorded speed, load and cleaning timing, then investigate abnormal trends rather than scheduling replacement from one reading. Use the pilot evidence to decide whether forecasting is reliable enough to plan intervention; until then, describe the work as condition monitoring, not proven predictive maintenance.
If a seal becomes displaced or grease could reach food, use the plant's stop/hold procedure and involve QA regardless of the vibration trend. If the data are inconsistent, improve the measurement method or retain scheduled checks. No successful outcome, failure reduction or payback is assumed.
Specification and enquiry: send the maintenance context
Copy and complete: “Component designation, machine position and quantity: __. Zone and contamination paths: __. Load, speed, running/idle duty and support arrangement: __. Washdown method, chemicals, concentration, temperature, dwell and rinse: __. Existing inspection and lubrication instructions: __. Failure/defect history and photographs: __. Measurement method, baseline and operating conditions: __. Planned inspection access, acceptance criteria and action owner: __. Material, cleaning/ingress evidence, applicable food-contact declarations and exact-design certificates required: __. Delivery country: __.”
Send these details to NHK
Send these details through this site's form so NHK can suggest a component and prepare a quote. Ask for the proposed item's permitted maintenance, mounting and cleaning conditions, rather than a general “washdown proof” label. Monitoring design and plant hygiene-release decisions may also require the machine builder, maintenance specialist and QA team; no diagnosis, response time or downtime guarantee is promised.